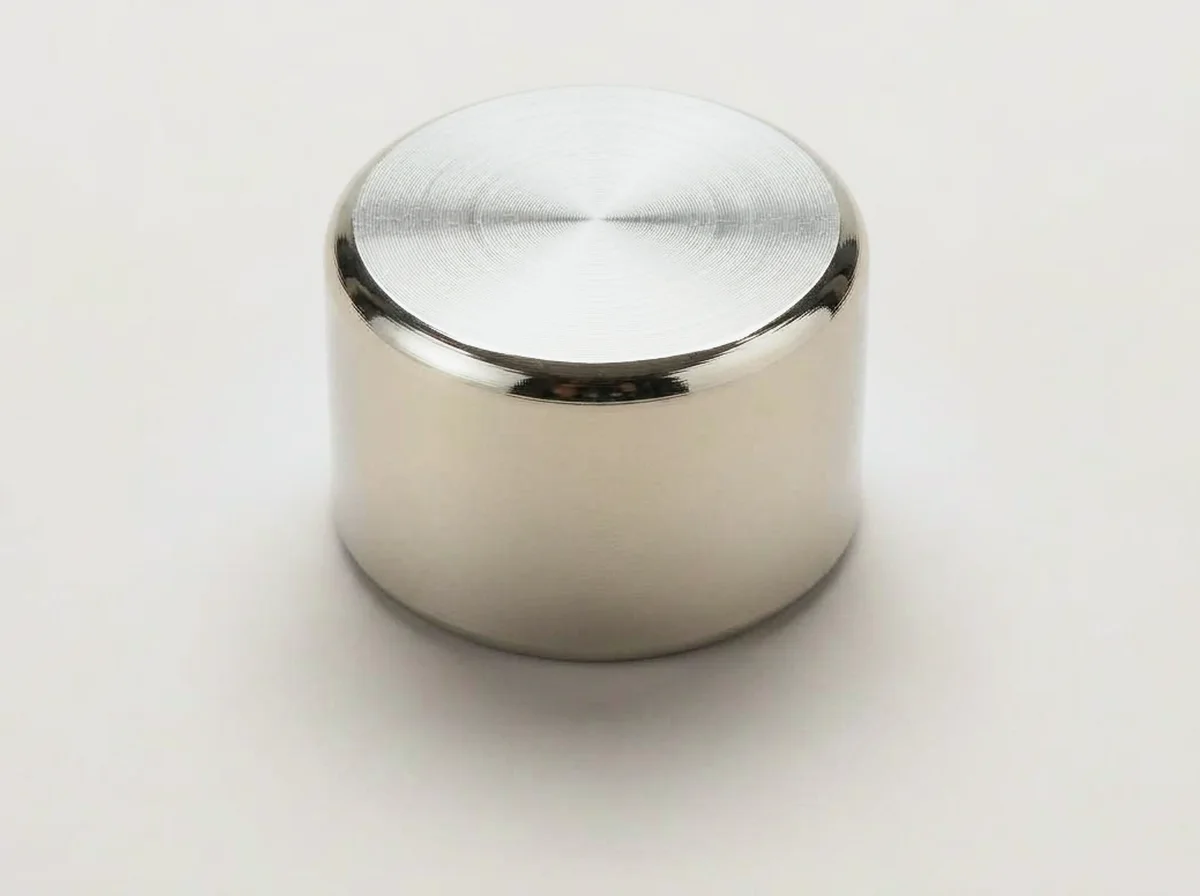
Electrolytic nickel plating
A hard, bright nickel layer deposited in an electrolytic bath. Corrosion and wear resistance with a clean appearance; an option for butterfly valve discs and expansion joint parts.
- THICKNESS
- 10–25 µm
- APPLICATION
- By a subcontractor
- TEMPERATURE
- −50 … +300 °C
- COST
Surface preparation
Surface preparation: degreasing and activation; on steel a copper interlayer if needed. Porosity decreases with thickness.
System and thickness
| SYSTEM | Thickness µm | Coats | Curing / process | Note |
|---|---|---|---|---|
| Fe/Ni 25 | 25 | 1 | Electroplating | Moderate environment; Emsal recommendation |
| Cu/Ni 10–15 (copper alloy) | 10–15 | 1 | Electroplating | Brass and bronze parts |
Thickness as dry film (µm). Emsal standard; binding values are set by the order specification.
Service temperature
The nickel layer withstands high temperature; the limit is set by the base material and the seal material.
Media suitability GENERAL TREND
Emsal assessment. The final choice is made from corrosion tables, taking concentration, temperature, chloride content and flow velocity into account.
Strengths and weaknesses
Strengths
- Hard, wear-resistant surface
- Clean, bright appearance
- Stable at high temperature
Weaknesses
- If there are pores, the steel underneath rusts (no cathodic protection)
- Pitting in chloride environments
- More expensive than zinc
Manufacturing and use
- ECONOMY
- Medium to high.
- MANUFACTURING METHODS
- Electroplating
- TYPICAL VALVE PARTS
- Disc (butterfly) · Stem · Expansion joint flange
Emsal practice
- APPLIED BY
- By a subcontractor
- METHOD
- Electrolytic nickel
- APPLIED TO
- Option for butterfly valves, gate valves and expansion joints; option for wafer and short-pattern swing check valves
Used in 10 Emsal products
- 001Wafer check valveCoatings (iron-carbon parts)
- 005Short pattern swing check valveCoatings (iron-carbon parts)
- 110Wafer butterfly valveCoatings (iron-carbon parts)
- 111Lug butterfly valveCoatings (iron-carbon parts)
- 130Flanged gate valveCoatings (iron-carbon parts)
- 310Metal bellows axial expansion jointCoatings (iron-carbon parts)
- 311Rubber expansion jointCoatings (iron-carbon parts)
- 312Double sphere rubber expansion jointCoatings (iron-carbon parts)
- 313Externally pressurized expansion jointCoatings (iron-carbon parts)
- 314V-flex expansion jointCoatings (iron-carbon parts)
Source: ISO 1456. Values compiled and verified by Emsal Vana; for binding values, refer to the current edition of the standard and the material certificate.